
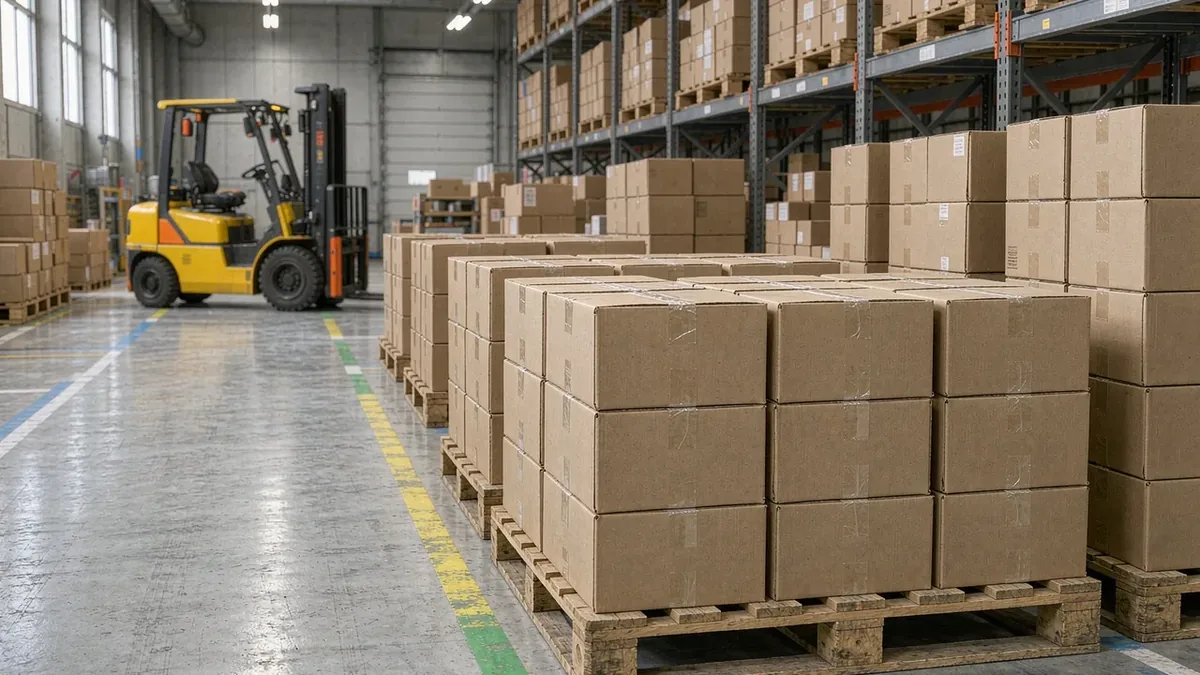
Warehouse and Inventory Control at a Cosmetic Factory
Brands audit the laboratory and the production hall and rarely spend much time in the warehouse. That is a mistake. The warehouse is where identity is established and retained, where the difference between a released and a quarantined material is enforced, and where traceability either works or does not.
Three Zones, Three Sets of Rules
A cosmetic warehouse holds three quite different streams, and each needs its own controls.
- Raw materials. Chemicals, oils, actives, fragrance compounds, pigments and powders. Many are subject to shelf life, temperature requirements or moisture sensitivity.
- Packaging components. Bottles, jars, tubes, pumps, droppers, caps, cartons and labels. Components have their own shelf life issues, particularly anything with a sprayed coating, an adhesive or a printed surface, and labels in particular have a defined storage life before the adhesive degrades.
- Finished goods. Released product awaiting shipment, which must be kept under the conditions the shelf life claim assumes and kept separate from anything not yet released.
Quarantine and Release Status
Nothing should be used before it has been released, and the warehouse should make that status visible without anyone having to consult a database. The standard mechanism is a physical status tag or label on every container, supplemented by a segregated physical area for quarantined goods. Three states are typical: quarantine, meaning received but not yet tested; released, meaning tested and approved for use; and rejected, meaning failed and awaiting disposition. A fourth state, on hold pending investigation, is worth having.
Where the physical status control is weak, the system depends entirely on individuals remembering, and the failure mode is predictable: an unreleased material is consumed into a batch that then has to be assessed, or a rejected material is used because the paperwork was ambiguous.
FIFO and FEFO
First in, first out is the baseline. First expired, first out is the more useful rule where materials carry expiry or retest dates, because it prevents a newer delivery from being consumed ahead of an older one that is closer to expiry. Practical enforcement requires either physical arrangement, with older stock placed in front, or a location-managed system where the warehouse management software directs the picker. Whichever is used, the receiving date and the supplier's batch number must be recorded against the location, otherwise neither rule can be applied.
Storage Conditions
Conditions matter more than many brands expect. Temperature-sensitive materials need a controlled area with a recorded temperature, and the records should be monitored for excursions rather than filed and forgotten. Hygroscopic powders need low humidity. Fragrance compounds and essential oils benefit from cooler storage away from light. Highly flammable materials, including alcohol and solvent-based products, need a separate, appropriately designed store. Humidity, temperature and light are all part of the storage specification for a reason, and the specification should be traceable to the material's supplier documentation or to the plant's own stability work.
Pest Control
A cosmetic warehouse attracts pests, particularly where plant-derived powders are stored. An integrated pest management programme covers inspection, monitoring with traps whose results are reviewed and trended, proofing of openings, and housekeeping standards. Bait stations and insect light traps are monitored, dated and signed. Absence of records is the finding an auditor will cite, even when the premises appear clean.
Stock Accuracy and Cycle Counting
A theoretical stock figure that does not match the physical stock causes real problems: purchasing buys what is not needed, production waits for what was thought to be available, and a batch record may state a quantity that was not in fact used. Cycle counting, where a portion of the inventory is counted on a rolling schedule rather than only during an annual shutdown, keeps the discrepancy small and identifies the causes: inaccurate picking, mislabelled locations, unrecorded damage. Discrepancies above a threshold should trigger an investigation, not an adjustment.
Traceability in Both Directions
Traceability must work forwards and backwards. Given a supplier's batch number, the plant should be able to list every finished batch that contains it. Given a finished batch number, the plant should be able to list every raw material and packaging component batch that went into it, along with the production date, the line and the personnel. This is the capability a recall depends on, and it should be testable in hours rather than days. A periodic traceability exercise, sometimes called a mock recall, is the honest way to find out whether it works.
What a Brand Should Ask
How are material statuses shown physically? What are the storage conditions and how are excursions handled? What is the cycle count frequency and the current accuracy? Can you run a traceability test on a recent batch and show me the output? A manufacturer working under ISO 22716 and GMP systems will answer all four from records. OEM COSMETICS ODM operates segregated and status-controlled stores with recorded conditions, cycle counting and a documented traceability procedure, and provides the material traceability sheet for each finished batch on request.
Talk to our team: WhatsApp +86 18709713948 · Email adon@oemcosmeticsodm.com · Website www.oemcosmeticsodm.com